
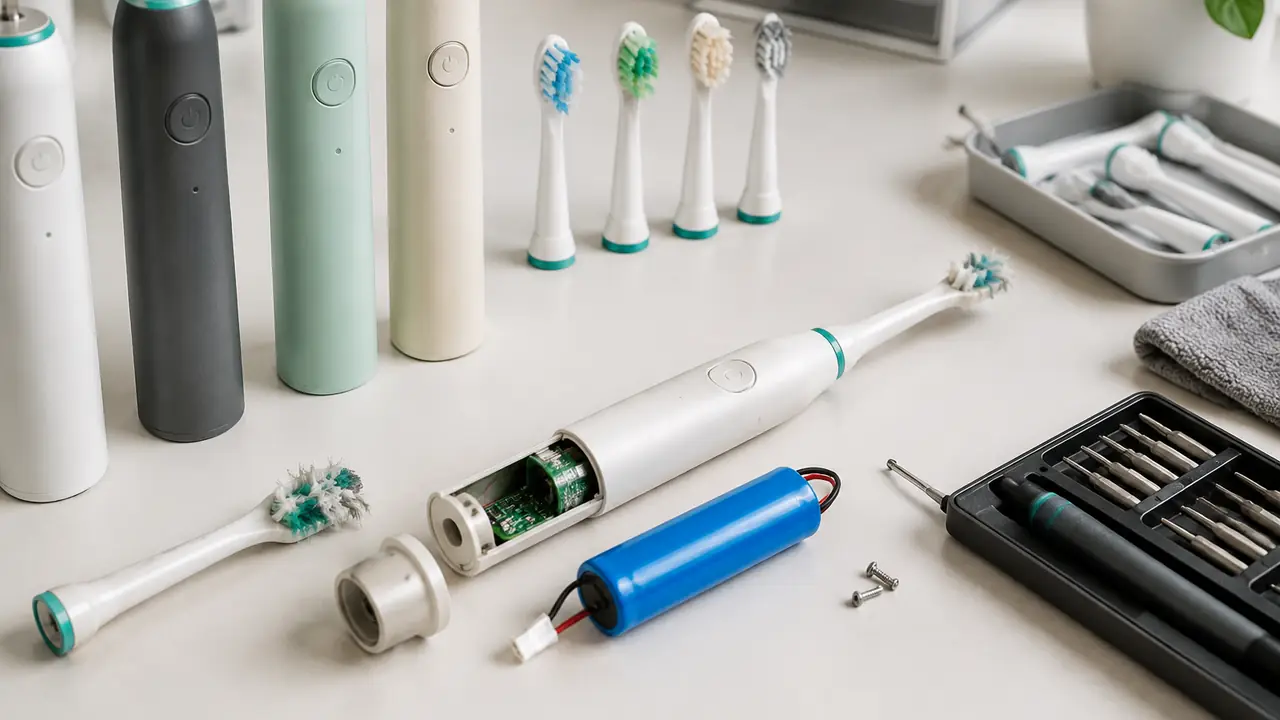
Triage before teardown
Three checks resolve most dead-handle reports before anyone opens anything. First, charge: a handle placed on a known-good dock or cable for a full charge window - hours, not minutes - comes back to life often enough that this step alone settles a large share of cases. Second, the travel lock: many handles ship with a lock engaged so they cannot switch themselves on in a box or a bag, and a user who never read the unlock gesture sees a brush that ignores every press. Third, on AAA-battery models, fresh cells fitted the right way round with clean contacts. Only when all three come back clear does the conversation move to the switch, the board or the motor.
The LED helps read the situation. No light at any press points one way; a brief blink that refuses to repeat points another; a handle that lights on the dock but not on the button is telling support that the power path works and the switch path does not. A one-line LED legend on the quick-start card converts those signals into answers.
The causes, in order of likelihood
Ordered from most to least common in practice across the category, the causes look like this. Frequencies differ by model and channel, so use the order as a triage sequence.
| Order | Cause | What the user sees | Brand-side lever |
|---|---|---|---|
| 1 | Flat or deep-discharged cell | No LED, no response, nothing on the dock | First-use charge instruction; protection thresholds |
| 2 | Travel lock engaged | Ignore every press; charges normally | Simple unlock gesture, printed on the card |
| 3 | AAA cells flat or reversed | Battery model silent after long storage | Polarity markings, spring contact design |
| 4 | Button or membrane failure | Clicks but no response, or no click at all | Button life spec; sealed button design |
| 5 | Board fault: solder joint, moisture | Charged, unlocked, still dead | Function test; post-drop function re-check |
| 6 | Motor failure | Rare; lights come on, head never moves | Motor life run-hours per the factory standard |
The travel lock: a feature that cuts both ways
Plants fit travel locks for good reasons. A handle packed in a suitcase or a shipping carton can press its own button against the box wall and arrive flat; retailers and marketplace sellers receive the complaint as dead on arrival, with the return cost attached. The lock closes that hole. The cost sits on the other side: every lock is a gesture a user must learn - a press-and-hold, a double press, a slide position - and every gesture that is not printed clearly becomes a will-not-start ticket instead.
The specification question is therefore not whether to have a lock but which form matches the audience. A single press-and-hold that both locks and unlocks is easy to print and hard to trigger by accident. A dedicated slide position is obvious but adds a part. Whatever the choice, the unlock gesture belongs on the box and the first card inside it, in the same words the support team uses. Programs that sell through marketplaces, where a dead-on-arrival review is public and expensive, have the strongest case for a lock and the strongest case for printing it.
Buttons, membranes and battery contacts
When the cause really is hardware, the button stack is where it usually lives. A press travels through a plastic cap, a silicone membrane dome and a board trace; any of the three can quietly stop conducting. Domes fatigue after many thousands of presses, which is why press-cycle life is a standard test item. Paste residue and moisture work in around the cap, which is why the button seal is part of the waterproofing conversation rather than a separate topic - a handle can pass an immersion test and still have a button that sticks in a steamy bathroom. The force and travel of the press are feel items, but they are written as numbers in the specification and checked on samples.
Battery models fail differently. Two AAA cells in a holder depend on leaf-spring contacts, and springs set wrong, cells fitted backwards or contacts corroded by humid storage all present as a dead brush. Contact material, spring pressure and moulded polarity markings are small specification lines that remove a whole complaint family. The battery toothbrush line covers the format, and battery vs rechargeable weighs the trade-offs; rechargeable handles move the same questions into the battery pack and its protection board.
What inspection catches before shipping
A will-not-start failure should never survive to a customer, and on a planned line it does not. A function check on each assembled unit - press, run, timer start - is the baseline item in the agreed plan. Button life is sampled by cycling presses to the agreed count, then re-checking response. Drop-tested samples are switched on again afterwards, because a solder joint that survives assembly can crack in the drop and fail in the customer's hand a month later. Battery models get a contact and polarity check, and rechargeable models inherit the cell incoming inspection and the UN 38.3 and IEC 62133-2 document review described in the charging note. Where the items sit in the plan is set out on the testing and inspection page, with the sampling logic on quality control.
The safety framework sits behind these items rather than replacing them. The appliance route runs under IEC/EN 60335-2-52 with the general rules of IEC 60335-1, or UL 859 for North America, verified per project. Those documents prove the design was examined; the line-level function checks prove this batch was built the way the design intended. A brand that keeps both - the standard's paperwork and the batch-level records - has an answer for the will-not-start claim that is evidence rather than apology.
Back to specification and inspection
A dead handle, traced to its root, is a short list of specification lines: the lock gesture and where it is printed, button force, travel and life, contact materials and polarity markings, protection thresholds on the pack. Each line costs little at the drawing stage and each removes a returns category. Agree them in the model specification, put the function, button-life and post-drop checks in the inspection plan, and confirm both in writing per program - reference quantities and schedules sit on MOQ and lead time, and a brief can start on the quote form.